Direct answer: Before sending material to a digital cutting machine supplier, define what will be cut, how the result will be measured, and what counts as a pass. At minimum, document the material, drawing revision, required operations, edge-quality standard, critical dimensions, small-feature requirements, material-holding expectations, repeatability, cycle-time method, and the evidence the supplier must return.
A test without written acceptance criteria usually becomes a demonstration. The supplier may show that the machine can cut the material, while the buyer actually needs to know whether the process can produce acceptable parts repeatedly under realistic production conditions.
Start with the production requirement, not the machine
A useful cutting test begins with the part and the downstream process. “Can this machine cut 5 mm felt?” is not enough. A better brief explains whether the felt contains adhesive, whether it is supplied by roll or sheet, which holes and corners matter, whether marks are allowed on the visible face, and how the cut part will be assembled.
| Test input | What to record | Why it matters |
|---|---|---|
| Material identity | Material name, supplier or grade, batch, measured thickness, density or hardness when relevant | Two materials with the same trade name may cut differently |
| Material format | Roll or sheet, width, usable area, surface direction, backing and protective film | Holding and feeding can change the result |
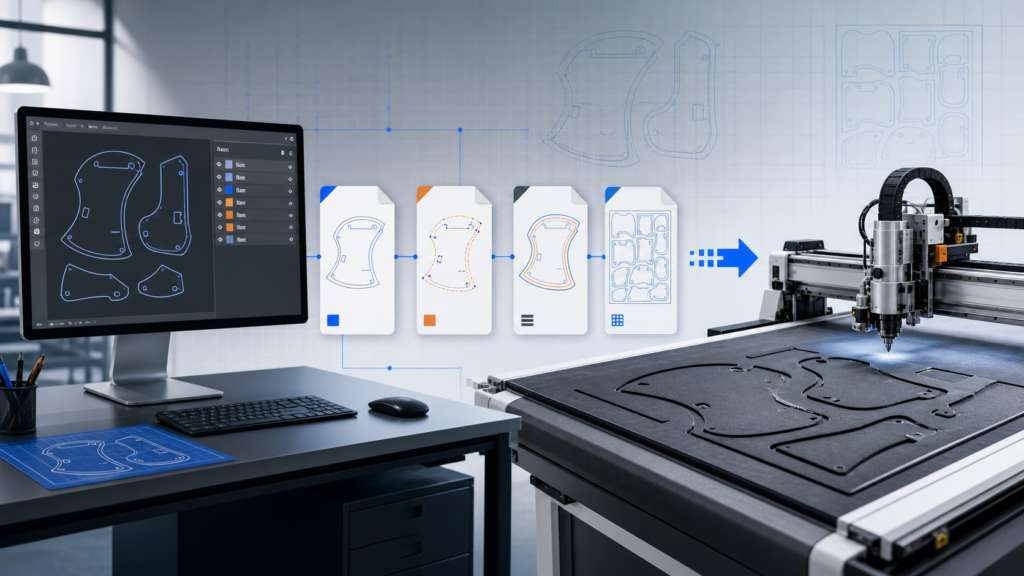
| Drawing | File format, units, scale, revision and critical features | Prevents testing an outdated or incorrectly scaled file |
| Required operations | Through-cut, kiss-cut, crease, V-cut, punch, drill or mark | Each operation may require a different tool and test method |
| Production context | Typical order size, variants, changeovers, daily demand and downstream process | A good sample is not automatically a good production workflow |
Define pass/fail criteria before the sample is cut
The acceptance table should distinguish measurable requirements from visual requirements. It should also identify who makes the final decision. If a dimension is critical to assembly, specify the measurement location and tool. If edge quality is visual, provide an approved reference sample or photographs that show acceptable and unacceptable results.
| Acceptance category | Questions to answer before testing | Evidence to request |
|---|---|---|
| Complete separation | Must the part release cleanly without manual trimming? | Top and bottom photographs plus an unedited removal video |
| Edge quality | Are loose fibers, compression, whitening, burrs or coating damage allowed? | Close-up images under consistent lighting and an approved reference |
| Critical dimensions | Which dimensions and holes affect assembly? | Measurement record with the method and instrument identified |
| Small features | What is the smallest inside corner, hole, notch or bridge? | A dedicated feature coupon, not only a large decorative shape |
| Surface condition | Are vacuum marks, scratches, pressure marks or contamination acceptable? | Visible-face photographs before and after cutting |
| Material stability | May the material stretch, rotate, lift or shift during the cut? | Video of the complete cut and comparison of repeated parts |
| Repeatability | How many consecutive parts must meet the same criteria? | Numbered samples and a result table for each run |
| Cycle time | Does timing include loading, registration, cutting, unloading and tool changes? | A clearly defined start and stop point, plus the job file |
Use representative samples, not only an easy piece
Send material that represents normal production variation. If your process uses different thicknesses, densities, coatings or backings, include the combinations that could change tool selection or holding. For natural leather, include realistic defects and irregular edges. For printed materials, include registration marks and normal print distortion. For corrugated board, identify board construction and flute direction.
The geometry should also be representative. A strong test file combines long straight cuts, tight curves, inside corners, small holes, notches and the actual operations required by the part. Do not let a simple logo or oversized shape become the only basis for a capital-equipment decision.
Separate capability testing from production validation
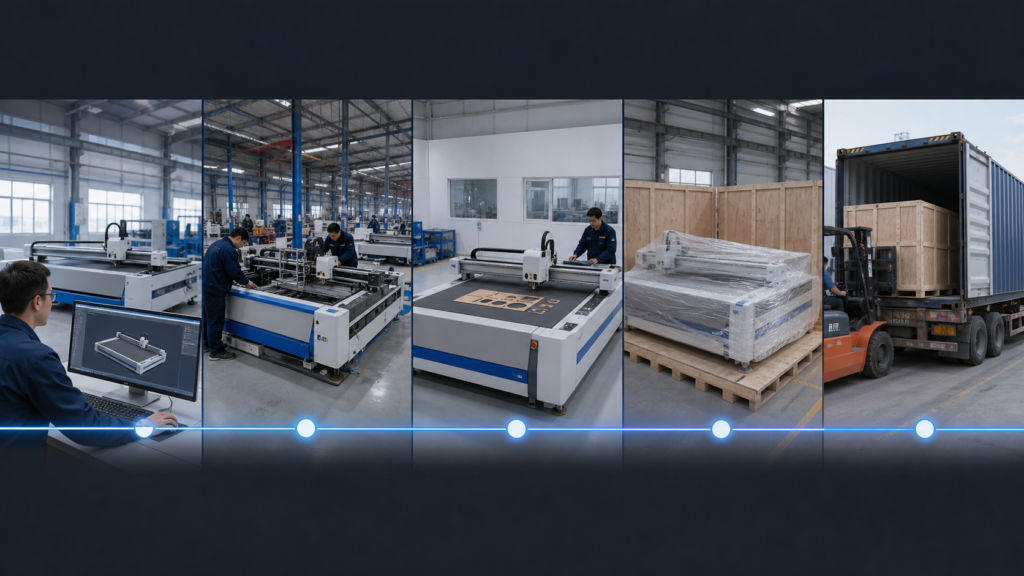
A pre-purchase material test answers whether a suitable tool and process can produce an acceptable part. A factory acceptance test goes further: it verifies the agreed machine configuration, safety functions, software, material handling, repeated cutting, documentation and other contracted requirements before shipment.
General FAT practice is based on defining the equipment, test conditions, required material and pass criteria in advance. The same principle applies to a digital cutter: do not wait until the machine is complete to decide what “acceptable” means.
What a supplier should return
- The original test request and drawing revision.
- Material identification and measured condition.
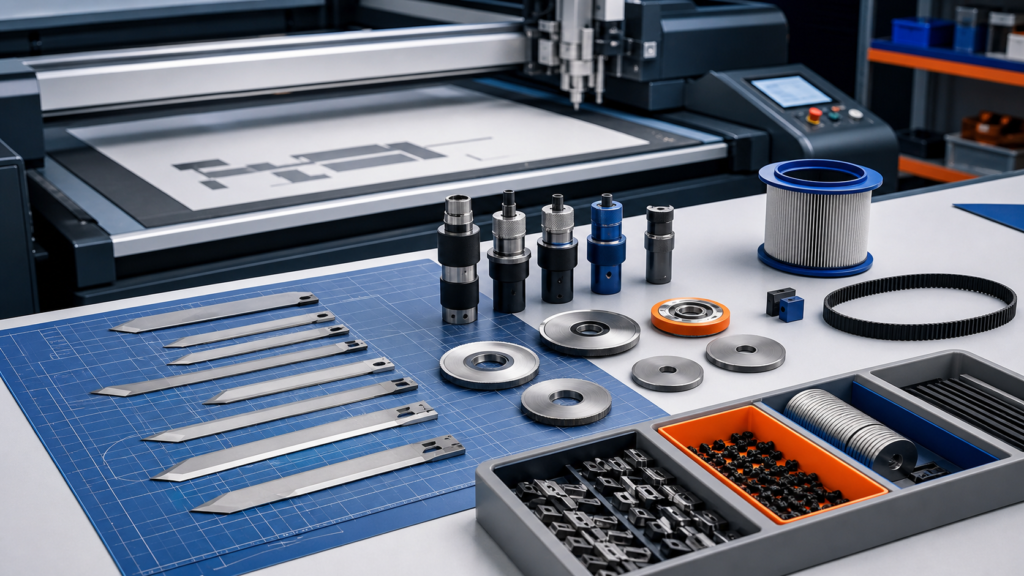
- The machine configuration and tool family used.
- Relevant process settings, without hiding failed trials.
- Numbered photographs of the top, bottom, edge and critical features.
- Results against every agreed acceptance criterion.
- Cycle-time definition and observed time, if requested.
- Exceptions, unresolved risks and recommended next test.
Common mistakes that make a cutting test unreliable
- Sending an unlabelled material sample with no technical information.
- Accepting a supplier-selected test shape that avoids difficult features.
- Changing the acceptance standard after seeing the result.
- Timing only the cutting path while excluding registration, loading or unloading.
- Judging one successful part without checking repeatability.
- Assuming one tool and setting will work across all batches or densities.
- Receiving a polished video but no raw samples, settings or inspection record.
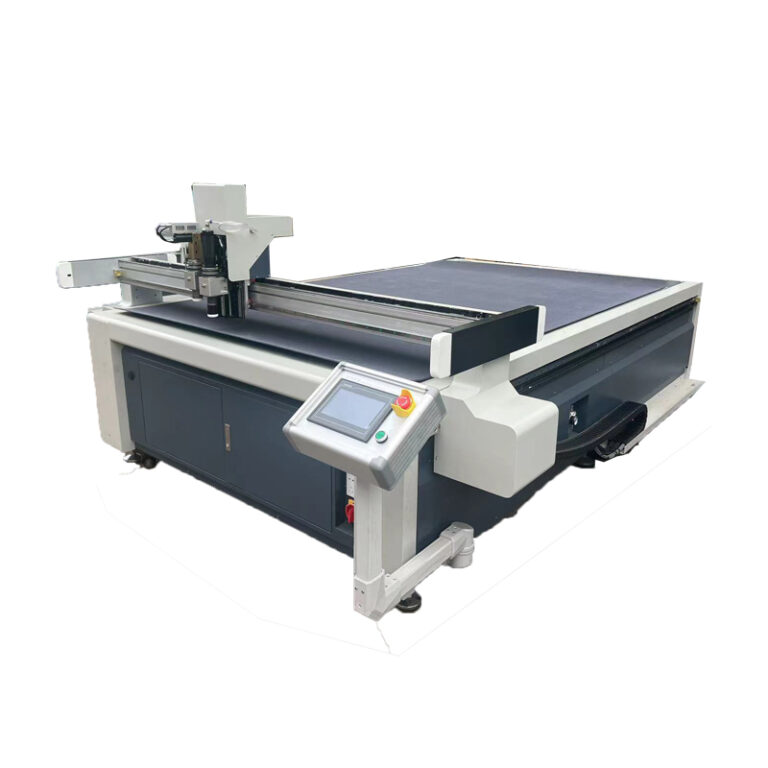
For the next stage of your evaluation, compare the material sample testing workflow, CNC cutter factory acceptance checklist, and JEKE application and material overview.
How JEKE can support a material test
JEKE provides material-based machine selection and supports customer sample cutting. To prepare a meaningful test, share the material type, thickness, usable width, drawing file, required operations, typical order mix and acceptance criteria. Tool selection and the final machine configuration should be based on the actual material and test result, not only on a generic material name.
Send your material and acceptance requirements to JEKE so the test can be planned around your production decision.
Frequently asked questions
Is a clean-looking sample enough to approve a digital cutter?
No. Visual appearance is one criterion. A buyer may also need to verify critical dimensions, complete separation, repeatability, surface condition, small features, material stability and the complete workflow.
Should the supplier choose the test settings?
The supplier can develop the process, but the buyer should define the result required. The final report should identify the tool and relevant settings so the result is traceable.
How many materials should be tested?
Test enough variants to represent the conditions that could change cutting behavior or configuration. There is no universal number. Prioritize the highest-volume material, the most difficult material and any material with a different backing, density, thickness or surface requirement.
Is a sample test the same as a factory acceptance test?
No. A sample test evaluates the material and process before final configuration. A FAT verifies the contracted machine and agreed functions before shipment.
Sources and further reading
- International Society of Automation: ISA-105 standards covering FAT, SAT and commissioning
- Krones: Factory acceptance test requirements and test-material planning
- U.S. Federal Acquisition Regulation: First article testing and approval principles
Last reviewed: August 20, 2026.